by Admin Admin No Comments

Phenolic Film Faced Plywood for Formwork: More Uses, Better Finish

Phenolic film faced plywood is engineered to deliver higher reuse cycles, cleaner concrete finishes and stronger moisture resistance compared with standard melamine film boards. This guide explains how phenolic film works in concrete formwork, where it delivers the most value, and how to use it correctly to maximise panel life.

What Is Phenolic Film Faced Plywood?

Phenolic film faced plywood is a structural plywood panel coated on one or both sides with a resin-impregnated phenolic film. The core veneers are bonded with exterior-grade glue and pressed under high temperature and pressure so that the film becomes a tough, durable surface layer suitable for repeated concrete pours.

The phenolic film itself is a kraft paper saturated with phenolic resin and cured to form a hard, chemically resistant coating. This coating protects the wood underneath from water, cement paste and abrasion during concrete placement, stripping and cleaning.

Compared with melamine or paper films, phenolic film offers a higher level of durability:

  • Phenolic film: High hardness, excellent abrasion resistance, very good water and chemical resistance.
  • Melamine film: Good surface quality but lower wear and moisture resistance than phenolic.
  • Paper or basic overlay: Suitable for light-duty use with limited reuse potential.

Key Advantages of Phenolic Film for Concrete Formwork

Upgrading from standard melamine to phenolic film changes how the panel behaves across multiple pours. The main benefits include superior resistance to water, chemicals and abrasion, and more consistent concrete surfaces over time.

Water and Chemical Resistance

Phenolic film creates a dense, non-porous surface that resists water penetration and alkaline attack from cement paste. This helps protect the glue line and core veneers against swelling and breakdown, especially in repeated wet–dry cycles or on sites with aggressive cleaning routines.

Abrasion Resistance and Surface Hardness

The cured phenolic layer has greater hardness and abrasion resistance than typical melamine films. It withstands contact with vibrators, tools and cleaning equipment better, slowing down surface wear and helping the panel retain its smoothness for more reuse cycles.

Better Concrete Finish and Fewer Patch Repairs

Because phenolic film maintains a smoother, more uniform surface over time, the concrete finish remains more consistent from pour to pour. This reduces patching, grinding and cosmetic repair work, especially on exposed surfaces where appearance matters.

Phenolic vs Melamine: Technical Comparison

A practical way to understand the benefit is to compare film types in terms of durability, typical reuse range and common applications.

Film Type Surface Durability Typical Reuse Cycles* Typical Applications
Paper / basic overlay Low – suitable for light-duty work ≈ 1–3 uses Small foundations, one-off jobs, temporary works
Melamine film Medium – decent finish, moderate wear resistance ≈ 4–8 uses (with proper handling) General building formwork, short to mid-term projects
Phenolic film High – excellent wear and moisture resistance ≈ 10–20 uses (with proper handling) High-rise, infrastructure, high-reuse formwork systems

*Actual reuse cycles will depend on glue system, core quality, concrete pressure, release agents, stripping methods, storage and climate.

Phenolic film also works well with proper edge sealing. When panel edges and cut edges are sealed correctly, the phenolic surface and sealed edges together form an effective barrier, reducing water uptake and extending panel life across multiple pours.

Impact on Reuse Cycles and Cost

The main reason contractors upgrade to phenolic film faced plywood is to increase reuse cycles and reduce total cost per use. The table below shows a simplified comparison between a melamine film panel and a phenolic film panel over a series of pours.

Panel Type Typical Reuse Range Estimated Cost per Use
Melamine film faced plywood 140 ≈ 6–8 uses (assume 7)
Phenolic film faced plywood 180 ≈ 12–18 uses (assume 15)

While the phenolic panel costs more per sheet, its lower cost per use and longer life usually reduce the total expense of formwork over 10–15 pours. Fewer panel replacements also mean less downtime, fewer emergency purchases, and a lower risk of surface defects that lead to rework.

On projects with many repetitive pours or on long-duration jobs, these savings can be significant, especially when labour, crane time and finishing work are included in the calculation.

Best Practices When Using Phenolic Film Faced Plywood

To get the full benefit of phenolic film, panels must be handled, treated and stored correctly. The following best practices help maximise reuse cycles and maintain surface quality.

Proper Edge Sealing and Cut Edge Treatment

Even with a robust phenolic surface, water can penetrate through unsealed edges and cuts. All panel edges should be factory-sealed, and any cut edges must be sealed on site using compatible paint or edge sealant. This reduces swelling, delamination and early failure at the edges.

Use Compatible Form Release Agents

Only use release agents that are compatible with phenolic film. Harsh or solvent-based products can soften or damage the film surface. Apply a thin, even layer and avoid pooling, which can mark the concrete or interfere with bond performance at edges and joints.

Cleaning and Storage Guidelines

After stripping, clean concrete residues with soft tools rather than sharp metal scrapers that can gouge the film. Allow panels to dry and store them flat on level supports, protected from standing water and direct weather. Good cleaning and storage practices are essential for achieving the upper end of the expected reuse range.

Where FOMEX GREENWOOD Phenolic Film Panels Fit Best

Phenolic film faced plywood from FOMEX GREENWOOD is designed for contractors and importers who need reliable performance in demanding concrete formwork applications. It is especially well suited to high-reuse formwork systems, core walls, main slabs, beams and columns in multi-storey projects.

These panels are typically produced in common formwork sizes and thicknesses suitable for most systems and can be matched to specific project requirements in terms of glue system, core composition and expected reuse cycles. They perform strongly in hot, humid and high-rainfall climates where moisture and temperature cycles are severe.

Need Help Selecting the Right Phenolic Film Panel?

FOMEX GREENWOOD engineers can recommend phenolic film faced plywood specifications based on your formwork system, project drawings and reuse targets.

Contact FOMEX Engineers →

Email: qc@fomexgroup.vn
☎ WhatsApp: +84 877 034 666

FAQs

Is phenolic film worth the extra cost?

For projects with multiple pours or where surface quality and reliability matter, phenolic film is usually worth the additional investment. Its higher reuse potential, lower cost per use, and reduced need for patching and panel replacement often result in lower total project cost compared with cheaper melamine film options.

How many more reuse cycles can I expect from phenolic film?

While exact numbers depend on glue, core quality and jobsite practices, phenolic film faced plywood can often deliver roughly double the reuse cycles of comparable melamine film panels when handled correctly. In many cases, this means moving from 6–8 uses to 12–18 uses or more.

Can phenolic film faced plywood be used for both walls and slabs?

Yes. Phenolic film faced plywood is suitable for walls, columns, slabs and beams, as long as the panel thickness and support spacing are chosen correctly for each application. Using the same panel type across different formwork zones can simplify logistics and inventory management.

How do I avoid damaging the phenolic surface?

Avoid using sharp metal tools directly on the film, use appropriate release agents, do not drag panels across rough surfaces, and store them flat and dry. Sealing cut edges and cleaning gently after each pour are key steps to protect the phenolic surface and maintain high reuse counts.

by admin admin No Comments

LUNAR NEW YEAR HOLIDAY NOTICE 2026

fomex tet 2026

Fomex Group would like to inform our valued partners and customers of our Lunar New Year holiday schedule:

🗓 Holiday Time: 14–22 Feb 2026
🏢 Back to Work: 23 Feb 2026

During this time, responses may be slower than usual. Normal operations will resume immediately after the holiday.

We sincerely thank you for your continued trust and cooperation.
Wishing you a prosperous Lunar New Year filled with success, happiness, and new opportunities.

by admin admin No Comments

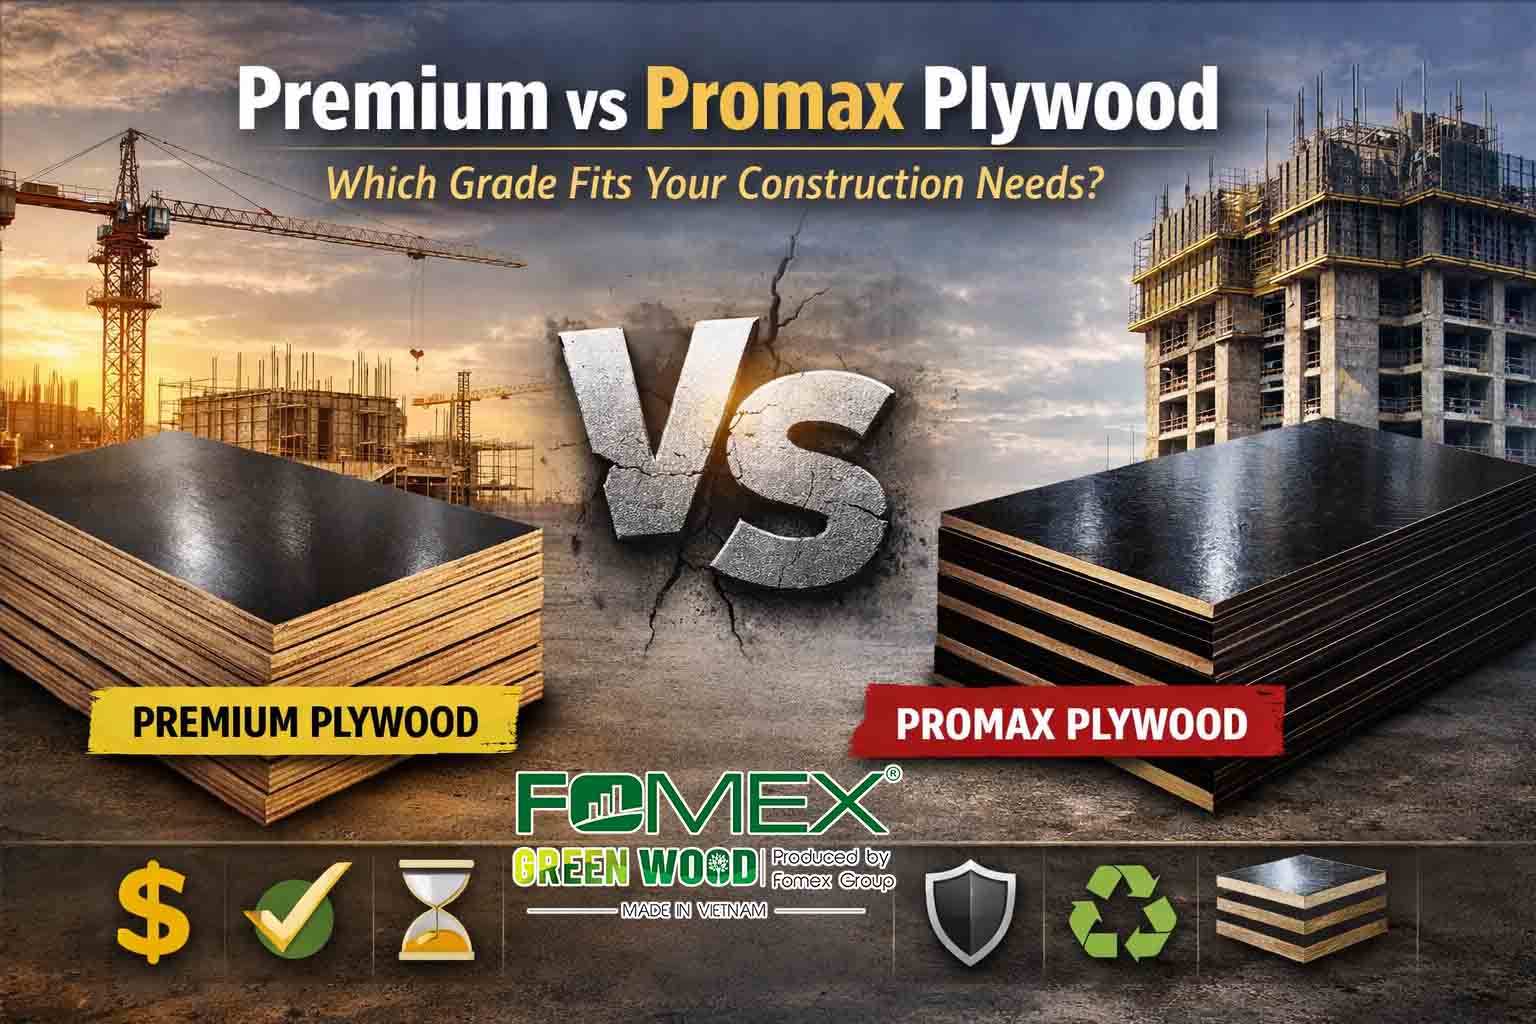
Which Grade Fits Your Construction Needs?

Choosing between Premium form plywood and Promax form plywood is a critical decision for contractors who care about reuse cycles, surface quality and overall project cost. This plywood grade comparison explains key technical differences and helps you match the right grade to each concrete formwork project.

Overview of Premium and Promax Formwork Plywood

In the FOMEX GLOBAL formwork range, Premium form plywood is designed as a high-quality, multi-use solution for demanding projects, while Promax form plywood represents the highest-performing grade, engineered for maximum reuse cycles and harsh jobsite conditions.

Both grades are film-faced panels built for concrete formwork, but they differ in glue content, boiling hours, film performance and target reuse ranges. Understanding these differences helps contractors and importers make smarter decisions on grade selection instead of relying on price alone.

A clear plywood grade comparison between Premium and Promax gives project managers and buyers a common language to discuss expectations around stiffness, surface quality, reuse cycles and risk control on site.

Technical Comparison: Premium vs Promax Formwork Plywood

The table below summarises key parameters for the two grades. Exact values depend on specification, but the relative positioning remains the same: Promax is optimised for higher durability and reuse potential.

Parameter Premium Form Plywood Promax Form Plywood
Typical glue system & boiling hours WBP melamine with high glue content, medium–long boiling hours for strong bond durability WBP melamine or phenolic with very high glue content, longest boiling hours for maximum bond strength
Film type and weight High-quality film faced plywood for smooth concrete finish and good wear resistance High-quality film, often with higher wear resistance for longer life under intense use
Core quality and construction Selected veneers with controlled core gaps, good balance between cost and performance Carefully selected veneers, tighter control of core gaps and veneer structure for maximum stability
Expected reuse range* Up to 12 uses with proper handling Up to 20 uses with proper handling
Moisture resistance and stability Strong resistance suitable for multi-cycle formwork in most climates Enhanced resistance for more cycles and tougher climates, especially under repeated wet–dry cycles

*Actual reuse cycles depend on glue type, project design, release agents, stripping methods, storage and climate conditions.

Choosing by Project Type and Budget

A smart plywood grade comparison considers not only technical data but also project duration, budget and reuse expectations. The “best” grade is the one that delivers the lowest risk and best cost-per-use for your specific job.

Short-Term Projects with Lower Reuse Targets – When Premium Is Sufficient

For short-duration projects, small commercial jobs or residential structures with moderate pour cycles, premium form plywood usually provides more than enough performance. It offers a robust film surface, good bond strength and stable cores at a price point that fits tighter budgets.

When expected reuse cycles fall in the 8–12 range and the project is not exposed to extreme climates, Premium is often the most cost-efficient solution. Contractors still get reliable performance without paying for the extra margin designed into Promax.

Long-Term Projects or High-Reuse Requirements – When Promax Is Recommended

For long-term projects, high-rise towers, large infrastructure or contractors using systematic formwork operations across multiple sites, promax form plywood becomes the stronger choice. Its glue and film systems are designed to withstand frequent cycling, aggressive schedules and heavy vibration.

When targets are in the 15–20 reuse range, or when formwork is expected to move from one project to the next, Promax helps minimise panel replacement, reduce risk of failure and support more predictable formwork planning across the company.

Climate and Exposure Conditions

Climate plays a major role in determining how quickly panels degrade. In hot, humid, coastal or high rainfall environments, repeated wetting and drying plus high temperature can stress both glue lines and film. Promax, with its higher glue content and more robust film, is better suited for these harsh conditions.

In moderate climates where panels can be kept relatively dry and protected, premium form plywood can still reach its intended reuse range. Understanding local climate and jobsite storage conditions is key to making the right grade choice.

Cost per Use Analysis: Premium vs Promax

A simple cost-per-use calculation often shows that high-performance panels can save money over the full project, even if they cost more per sheet. The example below assumes proper handling and average jobsite conditions.

Grade Approx. Panel Cost Typical Reuse Range Estimated Cost per Use
Premium form plywood 160 ≈ 8–12 uses (assume 10) ≈ 16 per use
Promax form plywood 200 ≈ 15–20 uses (assume 18) ≈ 11 per use

Over a 6–12 month project with many pours, the lower cost-per-use of Promax can offset its higher initial price, particularly when labour, downtime and claims from panel failure are included. For shorter projects with fewer cycles, Premium may still be the more economical option.

Decision Matrix for Contractors

The following points help contractors decide which grade to specify based on company profile, project type and risk tolerance.

Small vs Large Contractors

  • Small and mid-size contractors: Often prioritise cash flow and prefer premium form plywood for its lower upfront cost and solid performance on individual projects.
  • Large contractors and formwork specialists: Usually manage panels across multiple sites and benefit more from promax form plywood with higher reuse and better predictability.

Domestic vs Export-Funded Projects

  • Domestic projects: Premium is frequently sufficient when specifications are flexible and finish requirements are standard.
  • Export-funded or international standard projects: Promax is often preferred to meet stricter requirements on concrete finish, safety margins and documentation.

Safety and Quality Expectations

  • Projects with demanding safety requirements, heavy loads or complex geometry benefit from the extra margin built into Promax.
  • Where budgets are tight but reuse targets are moderate, Premium provides a strong compromise between performance and cost.

How FOMEX GREENWOOD Supports Grade Selection

Selecting between premium form plywood and promax form plywood is easier when you have access to technical support. FOMEX GREENWOOD engineers can review structural drawings, formwork layouts and reuse targets to recommend the most suitable grade and thickness.

Sample panels and trial pours can be arranged for key customers who want to validate performance before large-scale deployment. This approach reduces risk, aligns expectations and provides real data for your internal plywood grade comparison and procurement decisions.

Need Help Choosing Between Premium and Promax?

Share your project details, reuse targets and climate conditions, and FOMEX GLOBAL will recommend the right formwork plywood grade for your site.

Contact FOMEX Engineers →

Email: qc@fomexgroup.vn
☎ WhatsApp: +84 877 034 666

FAQs

What is the main difference between Premium and Promax plywood?

The main difference lies in reuse potential and durability. Premium form plywood is engineered for strong multi-use performance, while promax form plywood uses higher glue content, more robust film and tighter core control to support significantly higher reuse cycles and tougher jobsite conditions.

Is Promax always the better choice for high-rise projects?

Promax is often the preferred choice for high-rise projects because of its higher reuse potential and safety margin. However, if certain elements have low reuse counts or less demanding loads, Premium may still be suitable for those specific areas, depending on your formwork design.

How do I justify the higher cost of Promax to my client?

You can demonstrate that although Promax has a higher panel price, its lower cost-per-use, reduced replacement needs and lower risk of surface defects often decrease the total cost of concrete works. Including labour, delay and quality repair savings in your calculation makes the value of Promax clear.

Can I mix Premium and Promax in the same project?

Yes. Many contractors use premium form plywood for less critical or low-reuse elements and reserve promax form plywood for high-reuse zones such as core walls, main slabs or repeating structural bays. Mixing grades strategically can optimise both performance and budget.

👉 Looking for reliable Vietnamese plywood and wood solutions with consistent quality?
Contact: qc@fomexgroup.vn | https://fomexgroup.vn
WhatsApp: +84 877 034 666
by admin admin No Comments

How Many Reuses Can You Get from Concrete Formwork Plywood?

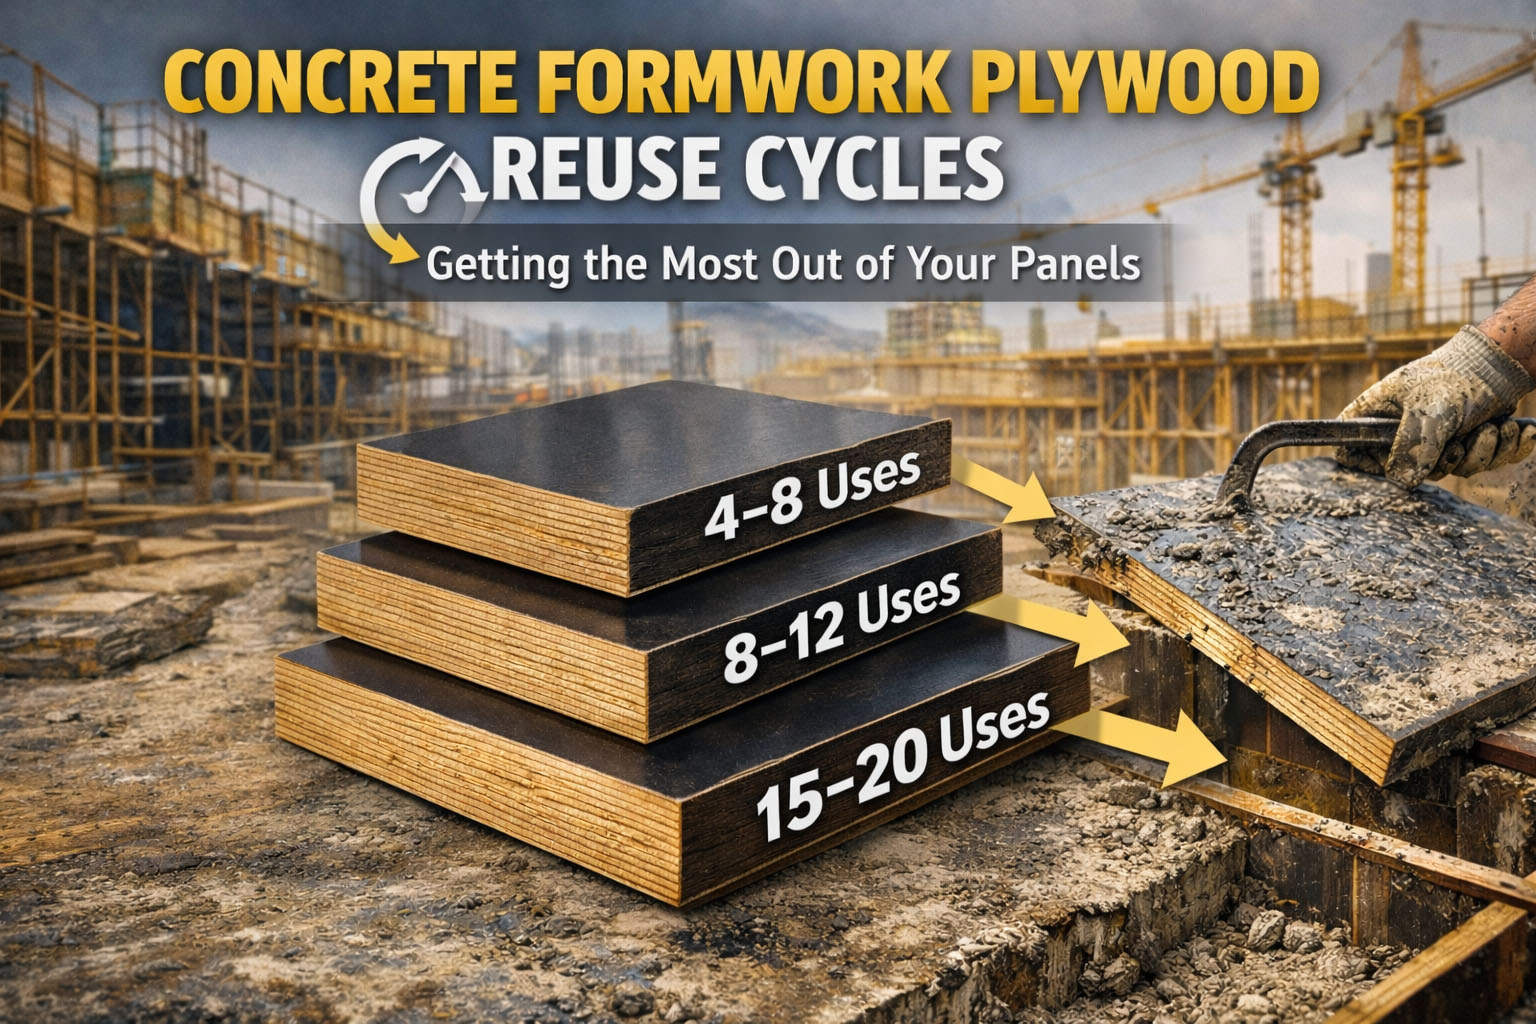
Understanding how many reuse cycles you can realistically expect from concrete formwork plywood is essential for safety, surface quality, and total project cost. This guide explains how glue type, boiling hours, film quality, moisture and handling practices influence reuse cycles from 2–3 up to 15–20 uses.

Plywood for Concrete Formwork: How Many Reuse Cycles Can You Expect?

What Is a “Reuse Cycle” in Concrete Formwork?

On a real jobsite, a “reuse cycle” means one complete sequence of assembling the form, pouring concrete, curing, stripping, and preparing the panel for the next pour. One sheet of plywood may be cut into several smaller pieces over time, but each pour that uses that material counts as one reuse cycle for that piece.

There is an important difference between structural reuse and aesthetic reuse. Structural reuse focuses on whether the panel can still safely carry load and resist concrete pressure; aesthetic reuse focuses on whether the surface is smooth enough to meet finish requirements. In many projects, panels remain structurally sound even when the surface no longer meets architectural expectations.

Stripping, cleaning and storage practices strongly influence how quickly a panel ages. Aggressive stripping tools, impact damage, and improper stacking can reduce the number of safe reuse cycles, even when the original glue system and film are designed for high performance.

Key Factors That Impact Reuse Cycles

The reuse potential of concrete formwork plywood does not depend on a single parameter. A realistic reuse estimate considers glue type and boiling hours, film quality, moisture content, climate and, most importantly, handling on site.

1. Glue Type and Boiling Hours

The glue system and boiling test rating determine how well the bond lines resist water, heat and cyclic loading. Panels designed for only a few uses often have lower glue content and shorter boiling times, while high-reuse panels use higher-grade resin and longer boiling tests to ensure durable bonding under demanding conditions.

2. Film Type and Film Weight

Film-faced panels for concrete formwork typically use either melamine or phenolic film. Melamine films are suitable for moderate reuse targets, while phenolic films offer higher abrasion resistance and better surface durability. Heavier film weights generally provide more protection against wear, impact and cleaning tools.

3. Moisture Content and Climate Conditions

Moisture content at the time of shipment and during storage affects both panel stability and glue performance. High humidity, frequent wetting and drying, and extreme temperature changes can reduce reuse cycles if panels are not properly conditioned and protected. Hot, dry climates and cold, humid regions each put different stress on the panel.

4. Handling, Stripping Tools and Storage

Even the best concrete formwork plywood will fail early if mishandled. Rough stripping with crowbars, dropping panels from height, cutting without sealing edges, or storing them in wet, uneven stacks will dramatically reduce the number of achievable reuse cycles. Careful handling and proper storage are often the biggest difference between hitting 15–20 uses and stopping at 5–7.

Reuse Ranges by Product Grade

Different formwork plywood grades are engineered for different reuse targets. The ranges below are indicative and assume correct handling, suitable glue systems, and proper film and core quality.

2–3 Reuse Cycles – Entry-Level Formwork Plywood

Entry-level formwork plywood is typically designed for small, short-term projects where only a few pours are required. Glue content and boiling hours are modest, and film quality is aimed at meeting basic formwork needs rather than long-term durability.

This category is suitable for minor foundations, one-off residential work, or temporary structures where the priority is low upfront cost. Contractors using this grade should not expect many reuses, especially under harsh jobsite conditions or aggressive stripping methods.

4–8 Reuse Cycles – Standard Formwork Plywood

Standard formwork plywood targets a balance between cost and performance. Glue systems are stronger than entry-level boards, and boiling hours are longer, supporting moderate resistance to moisture and repeated wet–dry cycles.

With proper handling and reasonable project conditions, contractors can typically achieve 4–8 reuse cycles. This range is common for general building projects, small commercial jobs, and contractors who want predictable performance without the cost of the highest-grade panels.

8–12 Reuse Cycles – Premium Formwork Plywood

Premium concrete formwork plywood uses higher-quality film, better core construction and longer boiling hours, providing significantly improved bond durability and surface wear resistance. These panels are designed for repeated cycling in demanding environments.

When combined with correct release agents and careful stripping and storage, premium panels can deliver 8–12 reuse cycles with consistent surface quality. They are well suited to mid- to long-duration projects, high-rise buildings, and contractors who prioritise reliable performance and reduced panel replacement rates.

15–20 Reuse Cycles – High-Performance Formwork Plywood

High-performance formwork panels are engineered for maximum reuse. They typically feature phenolic film, high glue content, robust core construction and the longest boiling times to ensure strong, durable bonding under repeated loading and exposure.

In well-managed projects with proper form oil, careful stripping tools, sealed edges and dry, flat storage, these panels can often achieve 15–20 reuse cycles or more. They are best suited to major infrastructure, long-duration high-rise projects and contractors running systematic formwork operations.

Best Practices to Maximize Reuse Cycles

The same plywood grade can deliver very different reuse results on different sites. Following a few best practices helps you get closer to the upper end of the expected reuse range.

1. Use Proper Form Oil and Release Agents

Apply compatible release agents evenly and avoid products that attack the film or glue line. Over-application or using the wrong oil can damage the surface, while under-application can cause concrete to stick and tear the film during stripping.

2. Avoid Impact Damage, Cuts and Nail Misuse

Do not drop panels from height or use them as temporary ramps without protection. Pre-drill or use appropriate fasteners to reduce splitting at edges. Cut panels with sharp blades and seal any exposed edges to protect the core from moisture.

3. Store Panels Dry, Flat and Supported

After stripping, clean panels carefully, allow them to dry, and stack them flat on level supports. Protect them from standing water and direct sunlight where possible. Good storage extends life, maintains flatness, and reduces the risk of delamination and warping.

When to Stop Reusing a Panel

It is important to know when a panel has reached the end of its safe life. Pushing panels beyond this point can compromise both structural performance and worker safety.

Visual Cues to Watch For

  • Severe edge damage, crushed corners or broken sections.
  • Delamination between veneers or visible core gaps opening at the edges.
  • Film peeling extensively, exposing raw veneer over large areas.
  • Excessive warping or bowing that prevents proper panel seating.

Safety Considerations

Even if the surface appearance is still acceptable, any sign that the panel may not safely carry the design loads is a reason to stop reusing it. For heavily loaded beams, high walls, or critical structural elements, it is better to retire questionable panels early than to risk failure during a pour.

Read More

Get Project-Specific Reuse Estimates

FOMEX GLOBAL  provide application-based estimates for concrete formwork plywood reuse cycles, considering your glue system, film type, climate and handling practices. Share your project details to receive tailored recommendations and cost-per-use scenarios.

Contact FOMEX GLOBAL→

Email: qc@fomexgroup.vn
☎ WhatsApp: +84 877 034 666

FAQs

How many times can phenolic film faced plywood be reused?

Under good handling and storage conditions, phenolic film faced plywood designed as a high-performance formwork panel can often achieve 15–20 reuse cycles. Actual results depend on glue type, core quality, release agents and site practices.

Can I increase reuse cycles by using better form oil?

Yes. Using a compatible, high-quality release agent and applying it correctly helps protect the film surface and reduce damage during stripping. This improves surface life and can increase the number of usable reuse cycles.

Why do some panels fail after only a few uses?

Early failure is often linked to low-grade glue systems, insufficient boiling hours, poor core construction, high moisture content, or aggressive handling and storage. Panels designed for 2–3 uses will not perform like premium or high-performance grades, especially under harsh conditions.

Are reuse cycles guaranteed by manufacturers?

Most manufacturers provide indicative reuse ranges based on laboratory testing and typical site conditions, not strict guarantees. Actual reuse cycles depend heavily on jobsite practices, structural design, climate and how the panels are treated between pours.

by admin admin No Comments

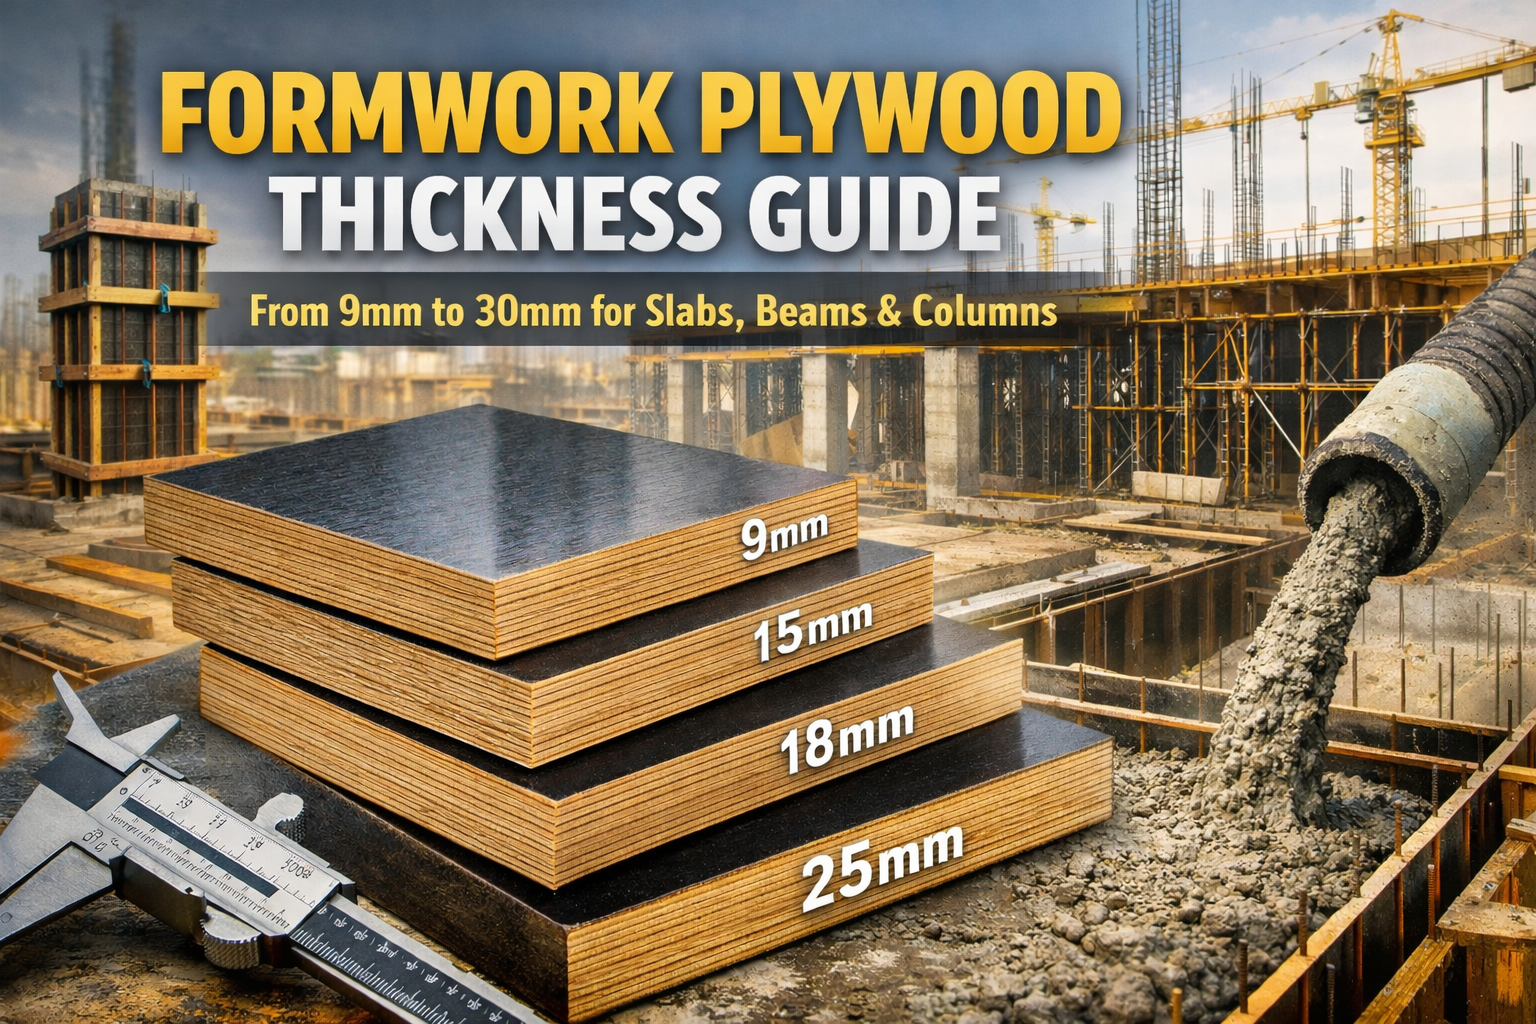
Formwork Plywood Thickness Selection Guide: 9mm to 30mm for Different Concrete Applications

Selecting the correct formwork plywood thickness is essential to balance structural safety, concrete finish quality, and overall project cost. This technical plywood thickness guide helps contractors and importers choose the right panel from 9mm to 30mm for slabs, beams, columns, walls, and foundations based on load conditions, spans, and reuse cycles.


Why Thickness Matters in Concrete Formwork

In concrete construction, formwork plywood thickness directly controls how panels respond to fresh concrete pressure, vibration, and repeated pours. Too thin, and you get excessive deflection, wavy surfaces, and blowouts; too thick, and you pay for unnecessary material cost and heavier handling without proportional performance gain.

The panel acts as a structural element under uniform and concentrated loads. Span between supports, concrete head pressure, and site equipment loads all influence how much the plywood will bend during pouring and curing. When bending exceeds acceptable limits, concrete surfaces become uneven, honeycombed, or misaligned.

From a cost perspective, thickness selection affects the cost-per-use of your formwork system. A well-designed plywood thickness guide aims to keep panels stiff enough to perform safely and cleanly, while also delivering predictable reuse cycles over the life of the project.

Key risks of wrong concrete formwork thickness:
• Uneven or wavy concrete surfaces that require grinding and patching
• Safety hazards from panel failure or formwork blowouts
• Increased rework and labour cost due to damaged panels
• Lower actual reuse cycles than planned, raising cost per pour

Key Factors That Influence Plywood Thickness

A practical plywood thickness guide never relies on a single “default spec.” Optimal thickness depends on the type of structure, concrete pressure, support system, and reuse targets for each project.

1. Type of Structure: Slab, Beam, Column, Wall, Foundation

Slabs behave like horizontal decks with uniform loads, beams and girders carry concentrated loads and high bending moments, while columns and walls are subjected to vertical hydrostatic pressure. Foundations and footings often see lower heights but irregular support from soil and temporary bracing.

2. Pour Height, Concrete Pressure and Rate of Pour

As pour height increases, so does lateral pressure on wall and column forms. Faster pour rates or high-slump concrete can further intensify pressure. For tall walls and high columns, thicker plywood is typically required to control deflection and maintain alignment at panel joints.

3. Support Spacing and Formwork System

Support spacing of joists, walers, and props is one of the most critical inputs for formwork plywood thickness selection. Closer spacing allows thinner panels; wider spacing demands thicker plywood. Traditional timber formwork, steel frames, and modular systems all create different span conditions that must be considered in design.

4. Reuse Expectations and Project Duration

Projects targeting 10–20 reuse cycles need panels with sufficient thickness, glue quality, and surface durability to survive repeated stripping, nailing, and handling. For one-off or low-reuse jobs, thinner panels can be acceptable if structural and safety criteria are still met.

Recommended Formwork Plywood Thickness by Application (9–30mm)

The table below summarises a practical plywood thickness guide for common concrete formwork applications. Values should be checked against local standards, engineering design, and the specific formwork system used on site.

Application Typical Thickness Range Typical Use Case Notes
Slab formwork 15–21 mm (up to 25 mm for long spans) Commercial and industrial slabs with moderate to high loads 18–21 mm widely used for medium spans; thicker panels for wide support spacing
Beam & girder formwork 18–25 mm Beam soffits, webs and sides under higher line loads Use higher thickness where beam depth and vibration levels are significant
Column & wall formwork 15–25 mm Vertical elements with hydrostatic concrete pressure 15–18 mm for low to medium heights; 18–25 mm for tall or fast pours
Foundations & footings 9–15 mm Strip footings, pads, low retaining structures Suitable where pour height is low and appearance is less critical

Slab Formwork Thickness (15–25 mm)

Slab formwork is typically subjected to uniform vertical load from fresh concrete, workers, and equipment. For tight support spacing and relatively thin slabs, 15–18 mm panels are common. For standard commercial spans, 18–21 mm is a widely accepted range that keeps deflection within limits while maintaining manageable weight.

Where spans are larger, loads are higher, or strict flatness is required for exposed finishes, 21–25 mm panels are often specified. In these conditions, the right concrete formwork thickness helps reduce rework on the slab surface and extends the number of reuse cycles.

Beam and Girder Formwork Thickness (18–25 mm)

Beams and girders concentrate load along narrower surfaces and create areas of higher bending stress on the formwork. In many projects, 18 mm is considered a practical minimum for beam soffits and sides, assuming support spacing is designed correctly and vibration is controlled.

For deeper beams, high concrete head, or heavy vibration, moving to 21–25 mm panels helps maintain panel rigidity, protect edges and corners, and reduce the risk of cracking or out-of-tolerance deflection. This is especially important when the beam soffit will remain visible or interface with other precision elements.

Column and Wall Formwork Thickness (15–25 mm)

Wall and column forms must resist vertical hydrostatic pressure, which increases with height and pour rate. For low walls or short columns, 15–18 mm plywood may be adequate when ties and walers are properly spaced. As height and pour rate increase, 18–21 mm or even 21–25 mm thickness may be required to control deflection and joint alignment.

Selecting the correct formwork plywood thickness for walls and columns prevents bulging, misaligned edges, and honeycombing at corners. Higher thickness and better core construction also improve edge durability during stripping and reuse.

Foundations and Footings Thickness (9–15 mm)

Foundations and footings generally have lower wall heights and shorter spans, allowing thinner panels in the 9–15 mm range when well supported. For simple strip footings, small pads, or temporary works where surface appearance is not critical, 9–12 mm plywood can be used with tight support spacing.

For slightly higher foundation walls or where handling damage is a concern, 12–15 mm can offer a better balance between cost and robustness. Even in these “rough” applications, quality veneer construction and appropriate glue remain important to avoid panel failure during concrete placement.

Thickness Selection Matrix for Global Markets

International buyers need a plywood thickness guide that works across different climates and building practices. The matrix below links application, thickness and suggested grade, with notes for major regions.

Application Thickness Range Suggested Grade Regional Considerations
Slab formwork 18–21 mm (up to 25 mm) Standard / Premium EU often prefers tighter deflection limits; Middle East projects focus on high reuse in hot conditions; US jobs vary by code and contractor practice.
Beam & girder formwork 18–25 mm Premium / Promax High-rise and infrastructure projects frequently require thicker and higher-grade panels for safety and longevity.
Column & wall formwork 15–25 mm Standard / Premium Cold, humid climates push for stable panels; hot, dry climates drive demand for glue and film systems that resist thermal stress.
Foundations & footings 9–15 mm Single / Standard Asia-Pacific markets often maximise cost efficiency using thinner panels where structural demands allow.

Common Mistakes When Choosing Formwork Thickness

  • Under-specifying thickness: Excessive deflection, wavy surfaces, panel breakage and higher safety risk during pours.
  • Over-specifying thickness: Up to 20–30% higher material cost, heavier handling, and no meaningful performance gain when supports are close.
  • Ignoring support spacing: Selecting panels without checking actual span between joists, walers and props leads to unexpected failures.
  • Confusing facing thickness with overall panel thickness: Focusing only on film or veneer while ignoring core thickness and construction quality.
  • Not considering reuse cycles: Choosing thin, low-grade panels for projects that actually need 10–20 uses, causing premature replacement.

5 Steps to Optimize Formwork Plywood Thickness

  • Calculate support spacing, slab or wall height, and expected concrete pressure.
  • Match pour rate and vibration method to the capacity of your selected thickness.
  • Define target reuse cycles (for example 2–3, 8–12, or 15–20 uses) and choose grade accordingly.
  • Verify plywood quality: veneer structure, glue system, edge sealing and moisture content.
  • Consult local formwork design standards and, where needed, structural engineers for final approval.

Read More

Get Expert Thickness Recommendations

FOMEX GREENWOOD engineers provide free, application-based formwork plywood thickness recommendations for concrete formwork projects worldwide. Share your slab, wall or column details, and our team will suggest suitable thickness, grade and reuse options.

Contact FOMEX Engineers →

Email: qc@fomexgroup.vn
☎ WhatsApp: +84 877 034 666

FAQs

What is the best plywood thickness for slab formwork?

For most commercial slab formwork with standard support spacing, 18–21 mm film-faced plywood is a reliable starting point. For long spans, heavy loads, or strict flatness requirements, moving to 21–25 mm panels improves stiffness and reduces the risk of visible deflection.

Can I use 12mm plywood for concrete formwork?

12 mm plywood can be used only in limited applications such as small foundations or very short spans with tightly spaced supports. It is generally not recommended for main slabs, beams, or tall walls because deflection and damage risk increase significantly under higher loads.

How does support spacing affect required plywood thickness?

The wider the distance between joists, walers or props, the more the panel must span, and the thicker it usually needs to be. Closer spacing allows thinner panels, while wider spacing often requires 18–21 mm or even 21–25 mm thickness to keep deflection within design limits and maintain safety.

Does a thicker panel always mean more reuse cycles?

Thicker panels provide better stiffness and mechanical strength, which can help increase potential reuse cycles, but thickness alone is not enough. Glue type, veneer structure, film quality, edge sealing, handling practices and climate all play major roles in how many safe reuses you actually achieve on site.

by admin admin No Comments

Why Plywood Shipments Get Rejected at Customs


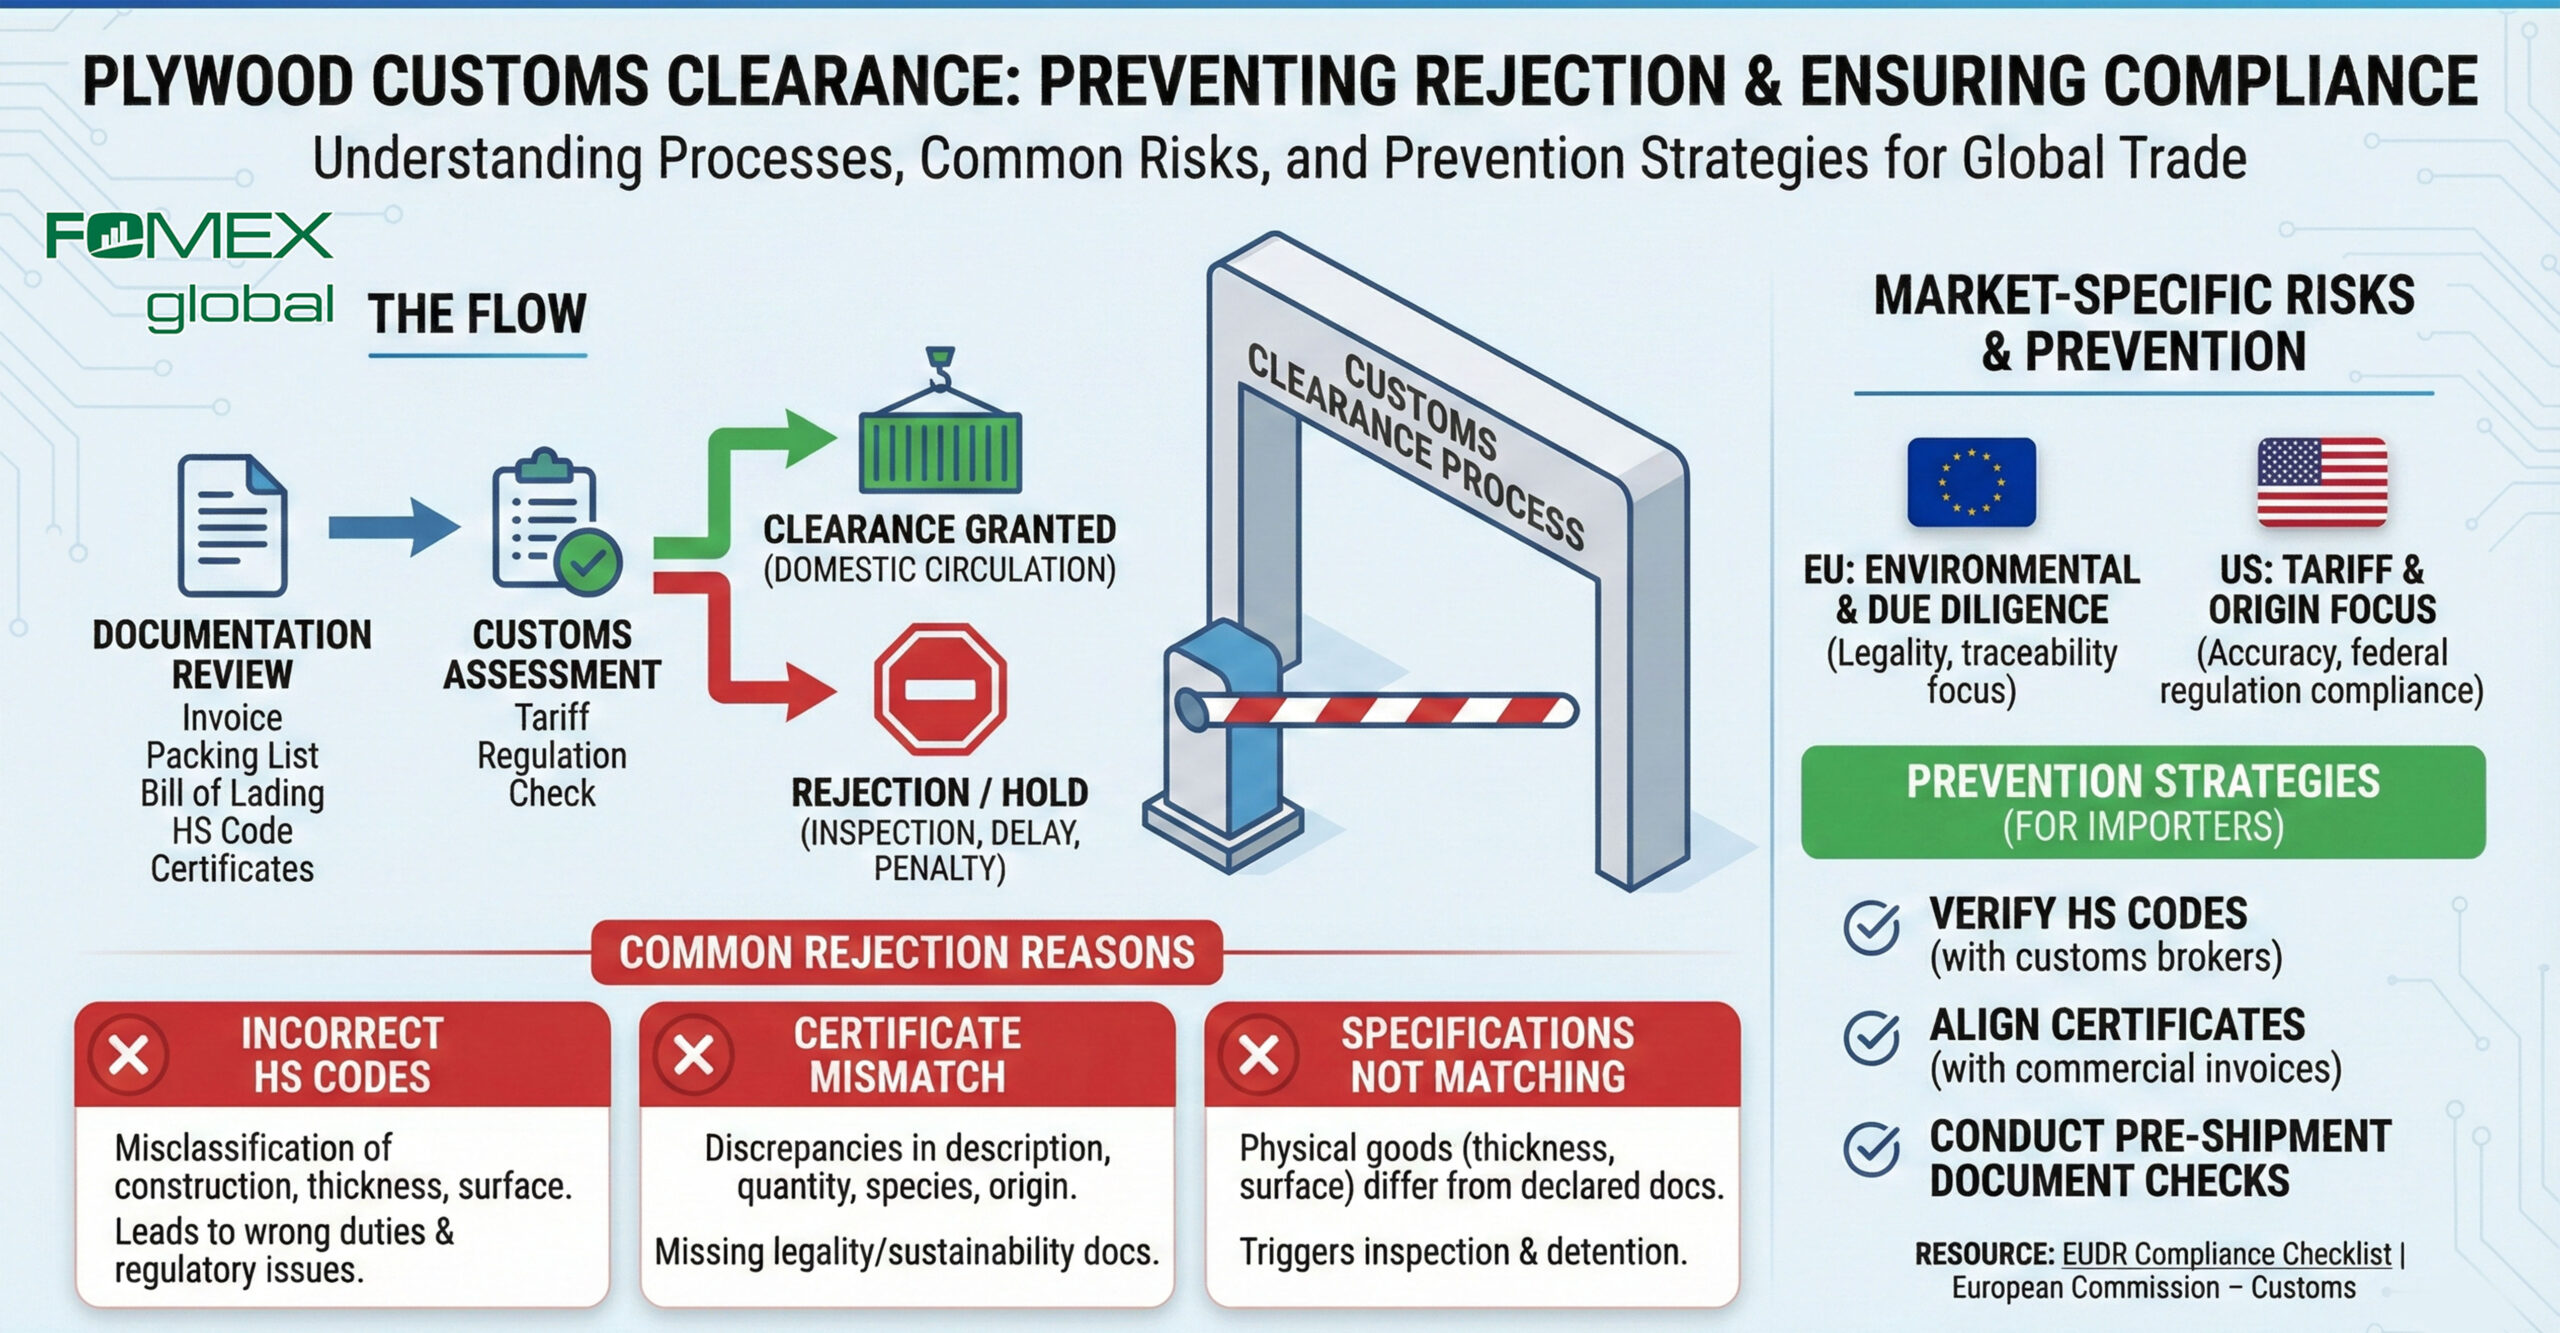
Customs rejection is one of the most costly risks in international plywood trade. Even when product quality is acceptable, documentation errors or regulatory mismatches can result in shipment delays, penalties, or refusal of entry. This article explains how plywood customs clearance works, the most common reasons shipments are rejected, and how importers can reduce compliance risk.

How Customs Clearance Works for Plywood

Customs clearance for plywood involves verifying that imported goods comply with tariff classification, product description, and regulatory requirements of the destination market. Authorities assess shipment documentation before releasing cargo for domestic circulation.

For plywood, clearance typically includes review of the commercial invoice, packing list, bill of lading, HS code declaration, and supporting certificates related to origin, legality, and environmental compliance. Any inconsistency between documents or between declared information and the
physical shipment may trigger inspection, delay, or rejection.

Common Reasons for Plywood Shipment Rejection

Incorrect HS Codes

Incorrect or inconsistent HS code classification is one of the most frequent causes of customs rejection. Plywood HS codes vary depending on construction, thickness, surface treatment, and intended use. Misclassification can lead to incorrect duty assessment or regulatory treatment, prompting customs authorities to hold or reject the shipment until discrepancies are resolved.

Certificate Mismatch

Certificate mismatches occur when information on certificates does not align with commercial documents or declared specifications. This includes discrepancies in product description, quantity, wood species, or country of origin. For regulated markets, missing or inconsistent legality and sustainability documentation significantly increases the risk of rejection.

Specifications Not Matching Documents

Customs authorities may inspect shipments to verify that physical goods match declared specifications. Differences in thickness, surface type, or panel construction can raise compliance concerns. Even minor inconsistencies may result in shipment detention while authorities assess whether misdeclaration has occurred.

Market-Specific Risks for Plywood Importers

Compliance requirements differ by market, increasing complexity for importers sourcing plywood internationally. In the European Union, customs clearance is closely linked to environmental and due diligence regulations. Documentation related to legality and traceability must be consistent and verifiable. In the United States, customs authorities focus on tariff classification accuracy, origin declaration, and compliance with federal import regulations. Inconsistent paperwork may trigger audits or extended inspections.

How Importers Can Prevent Customs Issues

Preventing customs rejection starts with structured export preparation rather than reactive problem solving at destination. Importers should ensure that all documents accurately reflect product specifications and regulatory requirements. Key preventive measures include verifying HS codes with customs brokers, aligning certificates with commercial invoices, and conducting pre-shipment document checks. Importers preparing for EU market entry may find this resource helpful:

EUDR Compliance Checklist for Plywood Importers

Official guidance on customs procedures is also available from the

European Commission – Customs

Avoid Customs Risks with FOMEX GLOBAL Export Support

Customs compliance requires experience, accuracy, and coordination between
exporters and importers. FOMEX GLOBAL supports buyers with structured
documentation, export-ready specifications, and compliance-focused processes
to reduce customs-related risks.

Contact FOMEX GLOBAL

Email: qc@fomexgroup.vn
☎ +84 877 034 666

by admin admin No Comments

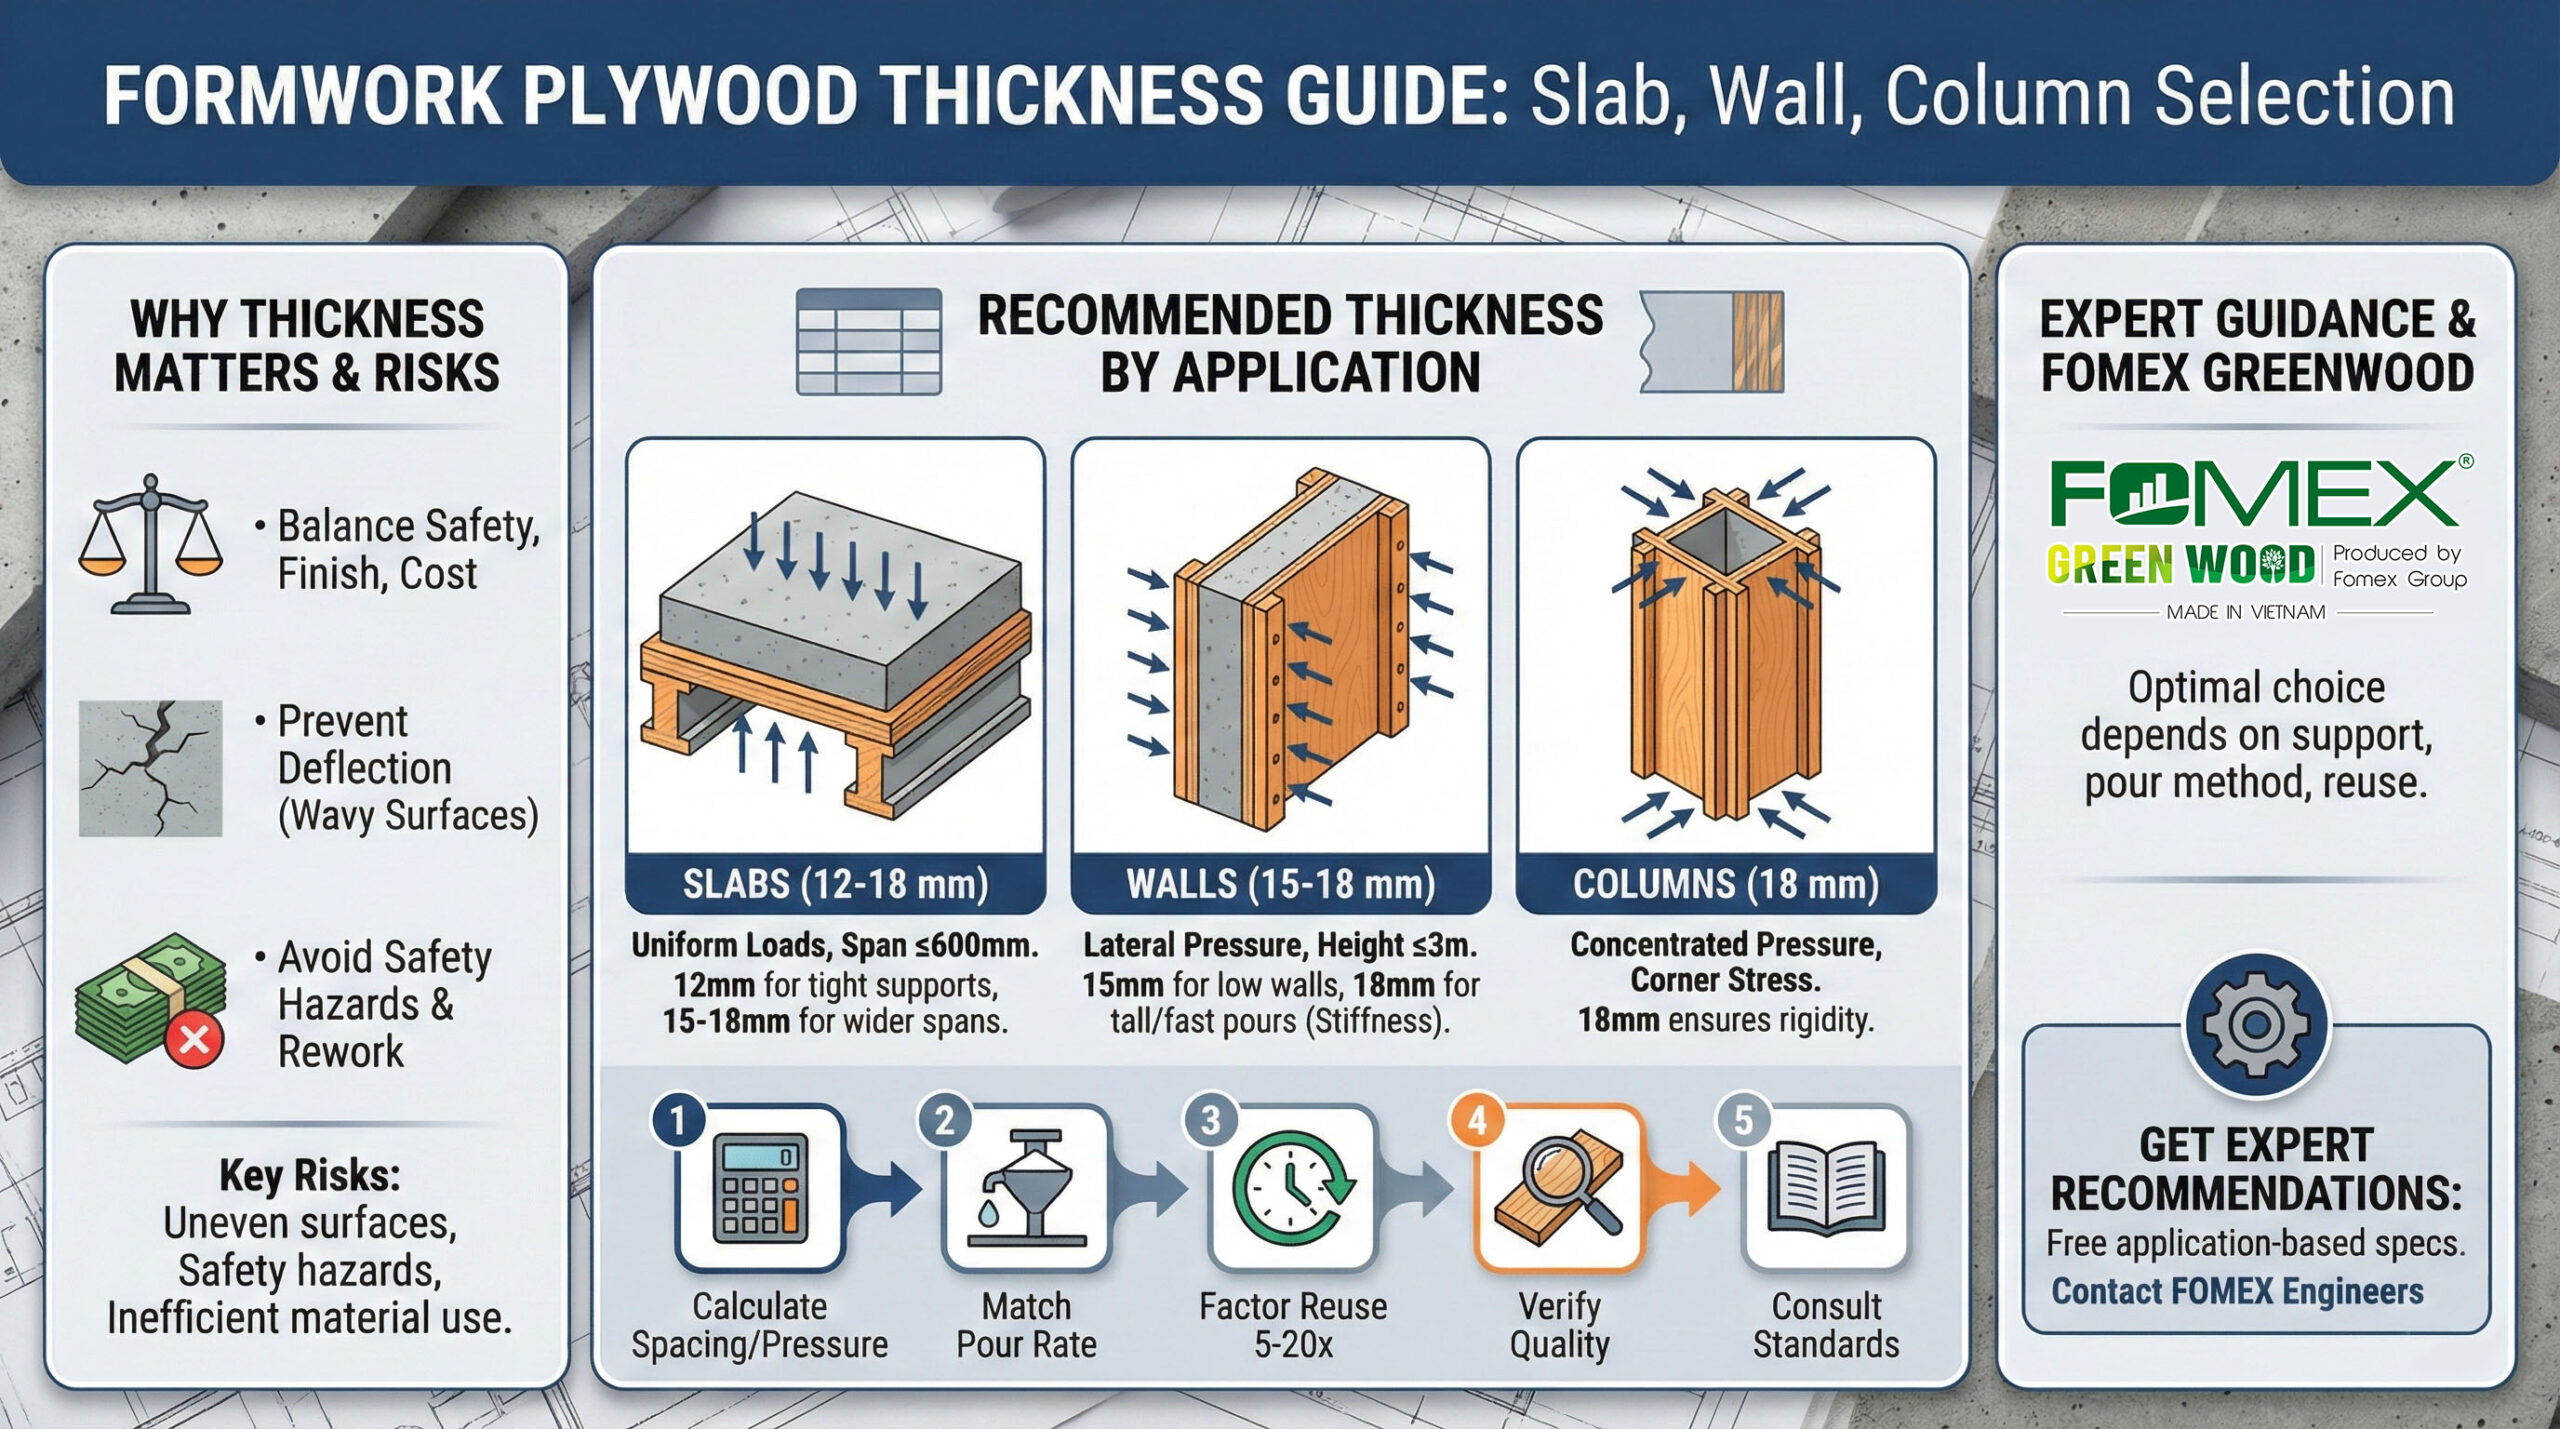
Formwork Plywood Thickness Selection Guide

Formwork Plywood Thickness Guide: Slab, Wall, Column Selection

Selecting correct plywood thickness for concrete formwork balances structural safety,
concrete finish quality, and project costs. This technical guide covers slabs, walls,
and columns based on load conditions, spans, and reuse cycles.

Formwork Plywood Thickness Guide

Why Formwork Plywood Thickness Matters

Plywood thickness determines panel response to fresh concrete pressure, vibration,
and repeated pours. Too thin = deflection → poor concrete surfaces. Too thick =
unnecessary costs and handling issues.

Key Risks:
Uneven surfaces, safety hazards, rework costs, inefficient material use.

As Vietnam plywood supplier, FOMEX GREENWOOD sees thickness often
treated as “default spec.” Optimal choice depends on support spacing, pour method,
and reuse targets.

Recommended Thickness by Application

Application Typical Thickness Key Factors Load Conditions
Slabs 12-18 mm Beam span ≤600mm, slab ≤200mm thick Uniform vertical load
Walls 15-18 mm Pour height ≤3m, lateral pressure High stiffness required
Columns 18 mm Corner stress, edge durability Concentrated pressure

Slab Formwork (12-18 mm)

Uniform loads over large areas. Use 12mm for tight supports (≤400mm span),
15-18mm for wider spans or high pours.

Wall Formwork (15-18 mm)

Lateral concrete pressure demands stiffness. 15mm for low walls, 18mm for
tall/fast pours to prevent bulging.

Column Formwork (18 mm)

High edge stress at corners. 18mm ensures rigidity during vibration and stripping.

Risks of Wrong Thickness Specification

  • Under-specify: Deflection → wavy surfaces, panel damage, safety risks
  • Over-specify: +30% material cost, heavier handling, no performance gain
  • Compromised concrete quality requiring grinding/polishing
  • Reduced reuse cycles (from 10→5 uses)

5 Steps to Optimize Thickness Selection

  • Calculate support spacing and concrete head pressure
  • Match pour rate/vibration to thickness capacity
  • Factor in expected reuse cycles (5-20 uses)
  • Verify plywood quality (veneer, glue, edges)
  • Consult formwork design standards

Read more

Get Expert Thickness Recommendations

FOMEX GREENWOOD engineers provide free application-based plywood specs
for your formwork projects worldwide.

Contact FOMEX Engineers →

Email: qc@fomexgroup.vn
☎ +84 877 034 666


by admin admin No Comments

Why Vietnam Is Emerging as a Global Plywood Sourcing Hub

Vietnam is rapidly establishing itself as the premier global plywood sourcing hub for 2026–2030.
Supply chain diversification, regulatory readiness, and manufacturing innovation are positioning Vietnam ahead of traditional markets.

Vietnam’s Strategic Advantages

💰 Competitive Cost Structure

Skilled workforce, automation and timber proximity deliver a superior cost‑to‑performance ratio while maintaining stable quality.

✅ Regulatory Compliance

FSC® certified, E0/E1, CARB Phase 2 and EUDR‑ready factories meet strict EU/US standards through 2030.

⚙️ Manufacturing Flexibility

Customization at scale, private labeling and fast prototyping so Vietnam adapts to your exact requirements.

⚠️ Reality Check: What to Watch

🏭 Factory Capability Variation
Technical sophistication differs widely between suppliers
📊 Quality Systems Maturity
QC processes range from basic to world-class
📋 Specification Precision
Detailed technical docs prevent misunderstandings
🚚 Peak Season Logistics
Plan capacity around Q3/Q4 export peaks

How to Select Your Vietnam Partner

✅ Essential Evaluation Criteria

  • Export track record to your target markets
  • Full certification portfolio (FSC/CARB/EUDR)
  • Transparent QC documentation
  • Capacity matching your volumes
  • Proven responsiveness to specification changes

📚 Strategic Resources

Ready to Secure Your Vietnam Sourcing Strategy?

FOMEX GREENWOOD delivers certified quality, full compliance, and strategic partnership
for importers targeting long-term plywood supply stability.

Partner with FOMEX GLOBAL Now

Email: qc@fomexgroup.vn | WhatsApp: +84 877 034 666

by admin admin No Comments

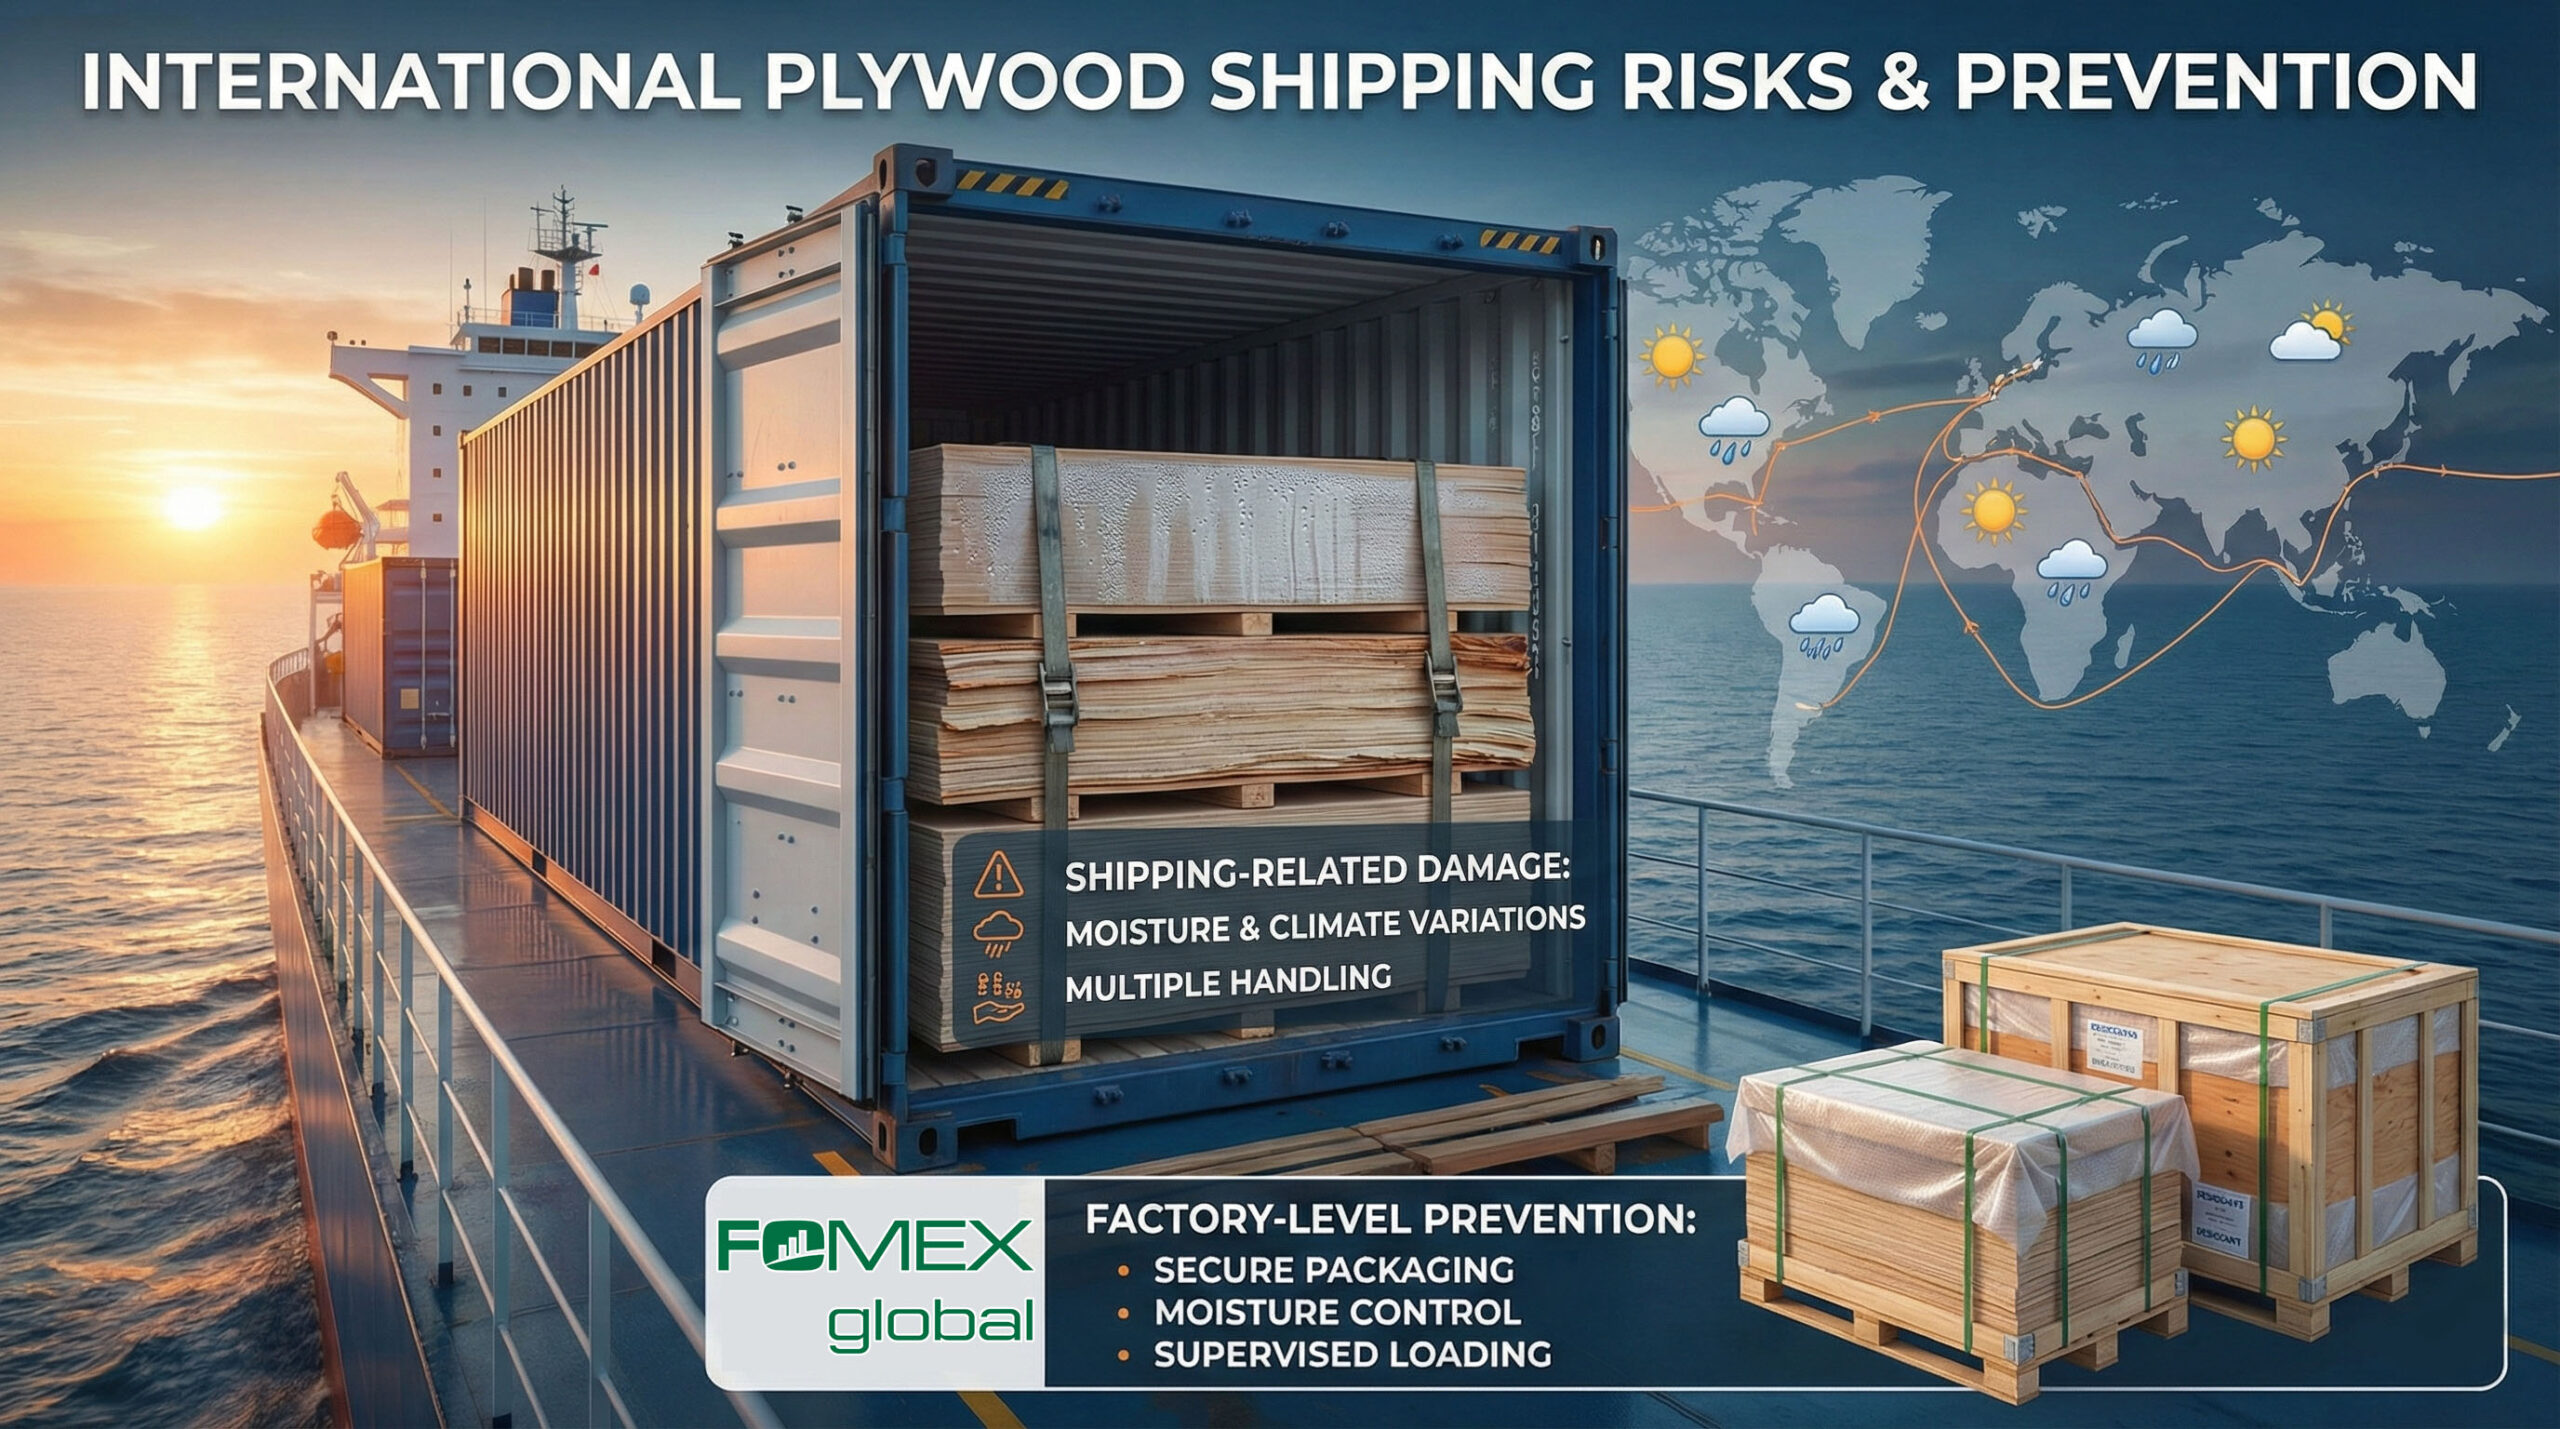
Plywood Damage During International Shipping

International shipping exposes plywood to long transit durations, climate variations,
and multiple handling stages. While plywood may leave the factory in compliant condition,
environmental exposure during transport can still create risks. This article explains
why shipping-related damage occurs — and how responsible manufacturers reduce these risks
before containers are sealed.

Why Shipping Damage Is a Common Issue

Plywood shipping damage is one of the most common concerns for global importers,
not because of manufacturing defects, but due to the complexity of international logistics.
Long sea routes, port dwell time, and climate transitions introduce variables that exist
beyond factory-controlled conditions.

As a Vietnam plywood exporter supplying Europe, the USA, and the Middle East,
FOMEX GLOBAL  frequently assists buyers in differentiating between product quality at
factory release and environmental exposure occurring after shipment.

Understanding this distinction is essential for accurate risk assessment, claim evaluation,
and realistic logistics planning.

Main Causes of Plywood Exposure During International Shipping

Container Moisture & Condensation

Moisture-related exposure during shipping is primarily linked to container environments
rather than manufacturing processes. Once plywood is packed, sealed, and loaded, containers
may pass through multiple climate zones where temperature fluctuations create condensation.

Such moisture accumulation typically develops during long ocean transit, port storage,
or delayed customs clearance. These conditions fall outside factory-controlled production
and inspection stages.

For plywood export from Vietnam, tropical humidity at origin combined with cooling at sea
increases condensation risk if logistics mitigation measures are not applied in advance.

Improper Loading and Weight Distribution

Mechanical stress during transport is often caused by incorrect loading practices rather
than panel quality. Uneven stacking, insufficient support, or unbalanced weight distribution
can lead to deformation or edge damage over time.

During extended voyages, vessel movement amplifies minor loading issues into visible damage
upon arrival.

Early Warning Signs Upon Arrival

Upon container arrival, importers should conduct immediate visual and olfactory inspection
to identify potential shipping-related exposure.

  • Surface discoloration associated with prolonged humidity exposure
  • Edge swelling or thickness variation after transit
  • Warping or panel distortion caused by environmental stress
  • Odor indicating moisture accumulation during transport or port storage

Early identification supports accurate documentation and helps determine whether exposure
occurred during transit or post-arrival handling.

Understanding the Difference Between Factory Quality and Transit Conditions

Many quality-related disputes arise from confusion between manufacturing quality and
logistics exposure. At factory level, plywood is produced, inspected, and packed under
controlled conditions according to export specifications.

Once containers are sealed, factors such as temperature fluctuation, humidity,
port congestion, and storage duration fall outside factory-controlled processes.

As a responsible Vietnam plywood supplier, FOMEX GLOBAL emphasizes
transparency by clearly defining what is controlled at factory level and what depends
on shipping environments.

How Manufacturers Can Minimize Shipping Risks Before Export

While no exporter can control every environmental variable during international shipping,
preventive measures at factory level significantly reduce logistics-related risks.

Controlled Moisture Content Prior to Packing

Plywood is conditioned and inspected to ensure moisture levels are within specified limits
before packing. Stable moisture content helps panels withstand environmental changes during
transit.

Export-Grade Packaging and Protection

Proper export packaging includes pallet bases, protective wrapping, reinforced edges,
and secure strapping to reduce movement and vibration.

Packaging principles and buyer expectations are further explained here:

MOQ, Lead Time & Packaging Standards

Container Inspection and Supervised Loading

Prior to loading, container condition is inspected for cleanliness, dryness, and structural
integrity. Loading is supervised to ensure proper stacking and balanced weight distribution.

These practices align with international shipping safety guidance published by the

International Maritime Organization (IMO)

Why Factory-Level Prevention Matters More Than Post-Arrival Claims

Cargo insurance may provide financial coverage, but it does not eliminate project delays,
handling costs, or reputational impact. Preventive preparation at factory level is more
effective than corrective action after arrival.

As a sustainable plywood exporter, FOMEX GLOBAL treats logistics risk
management as an extension of product quality — not a separate responsibility.

Learn How FOMEX Minimizes Shipping Risks Before Export

While international shipping always involves environmental variables, FOMEX GLOBAL
applies factory-level preventive measures to reduce moisture-related and mechanical risks
before containers are sealed and shipped.

Contact FOMEX GLOBAL

Email: qc@fomexgroup.vn  |   WhatsApp: +84 877 034 666

by admin admin No Comments

How to Read a Plywood Specification Sheet: Details Importers Often Miss

Learn how to read a plywood specification sheet, avoid common importer mistakes, and understand key plywood technical data clearly.
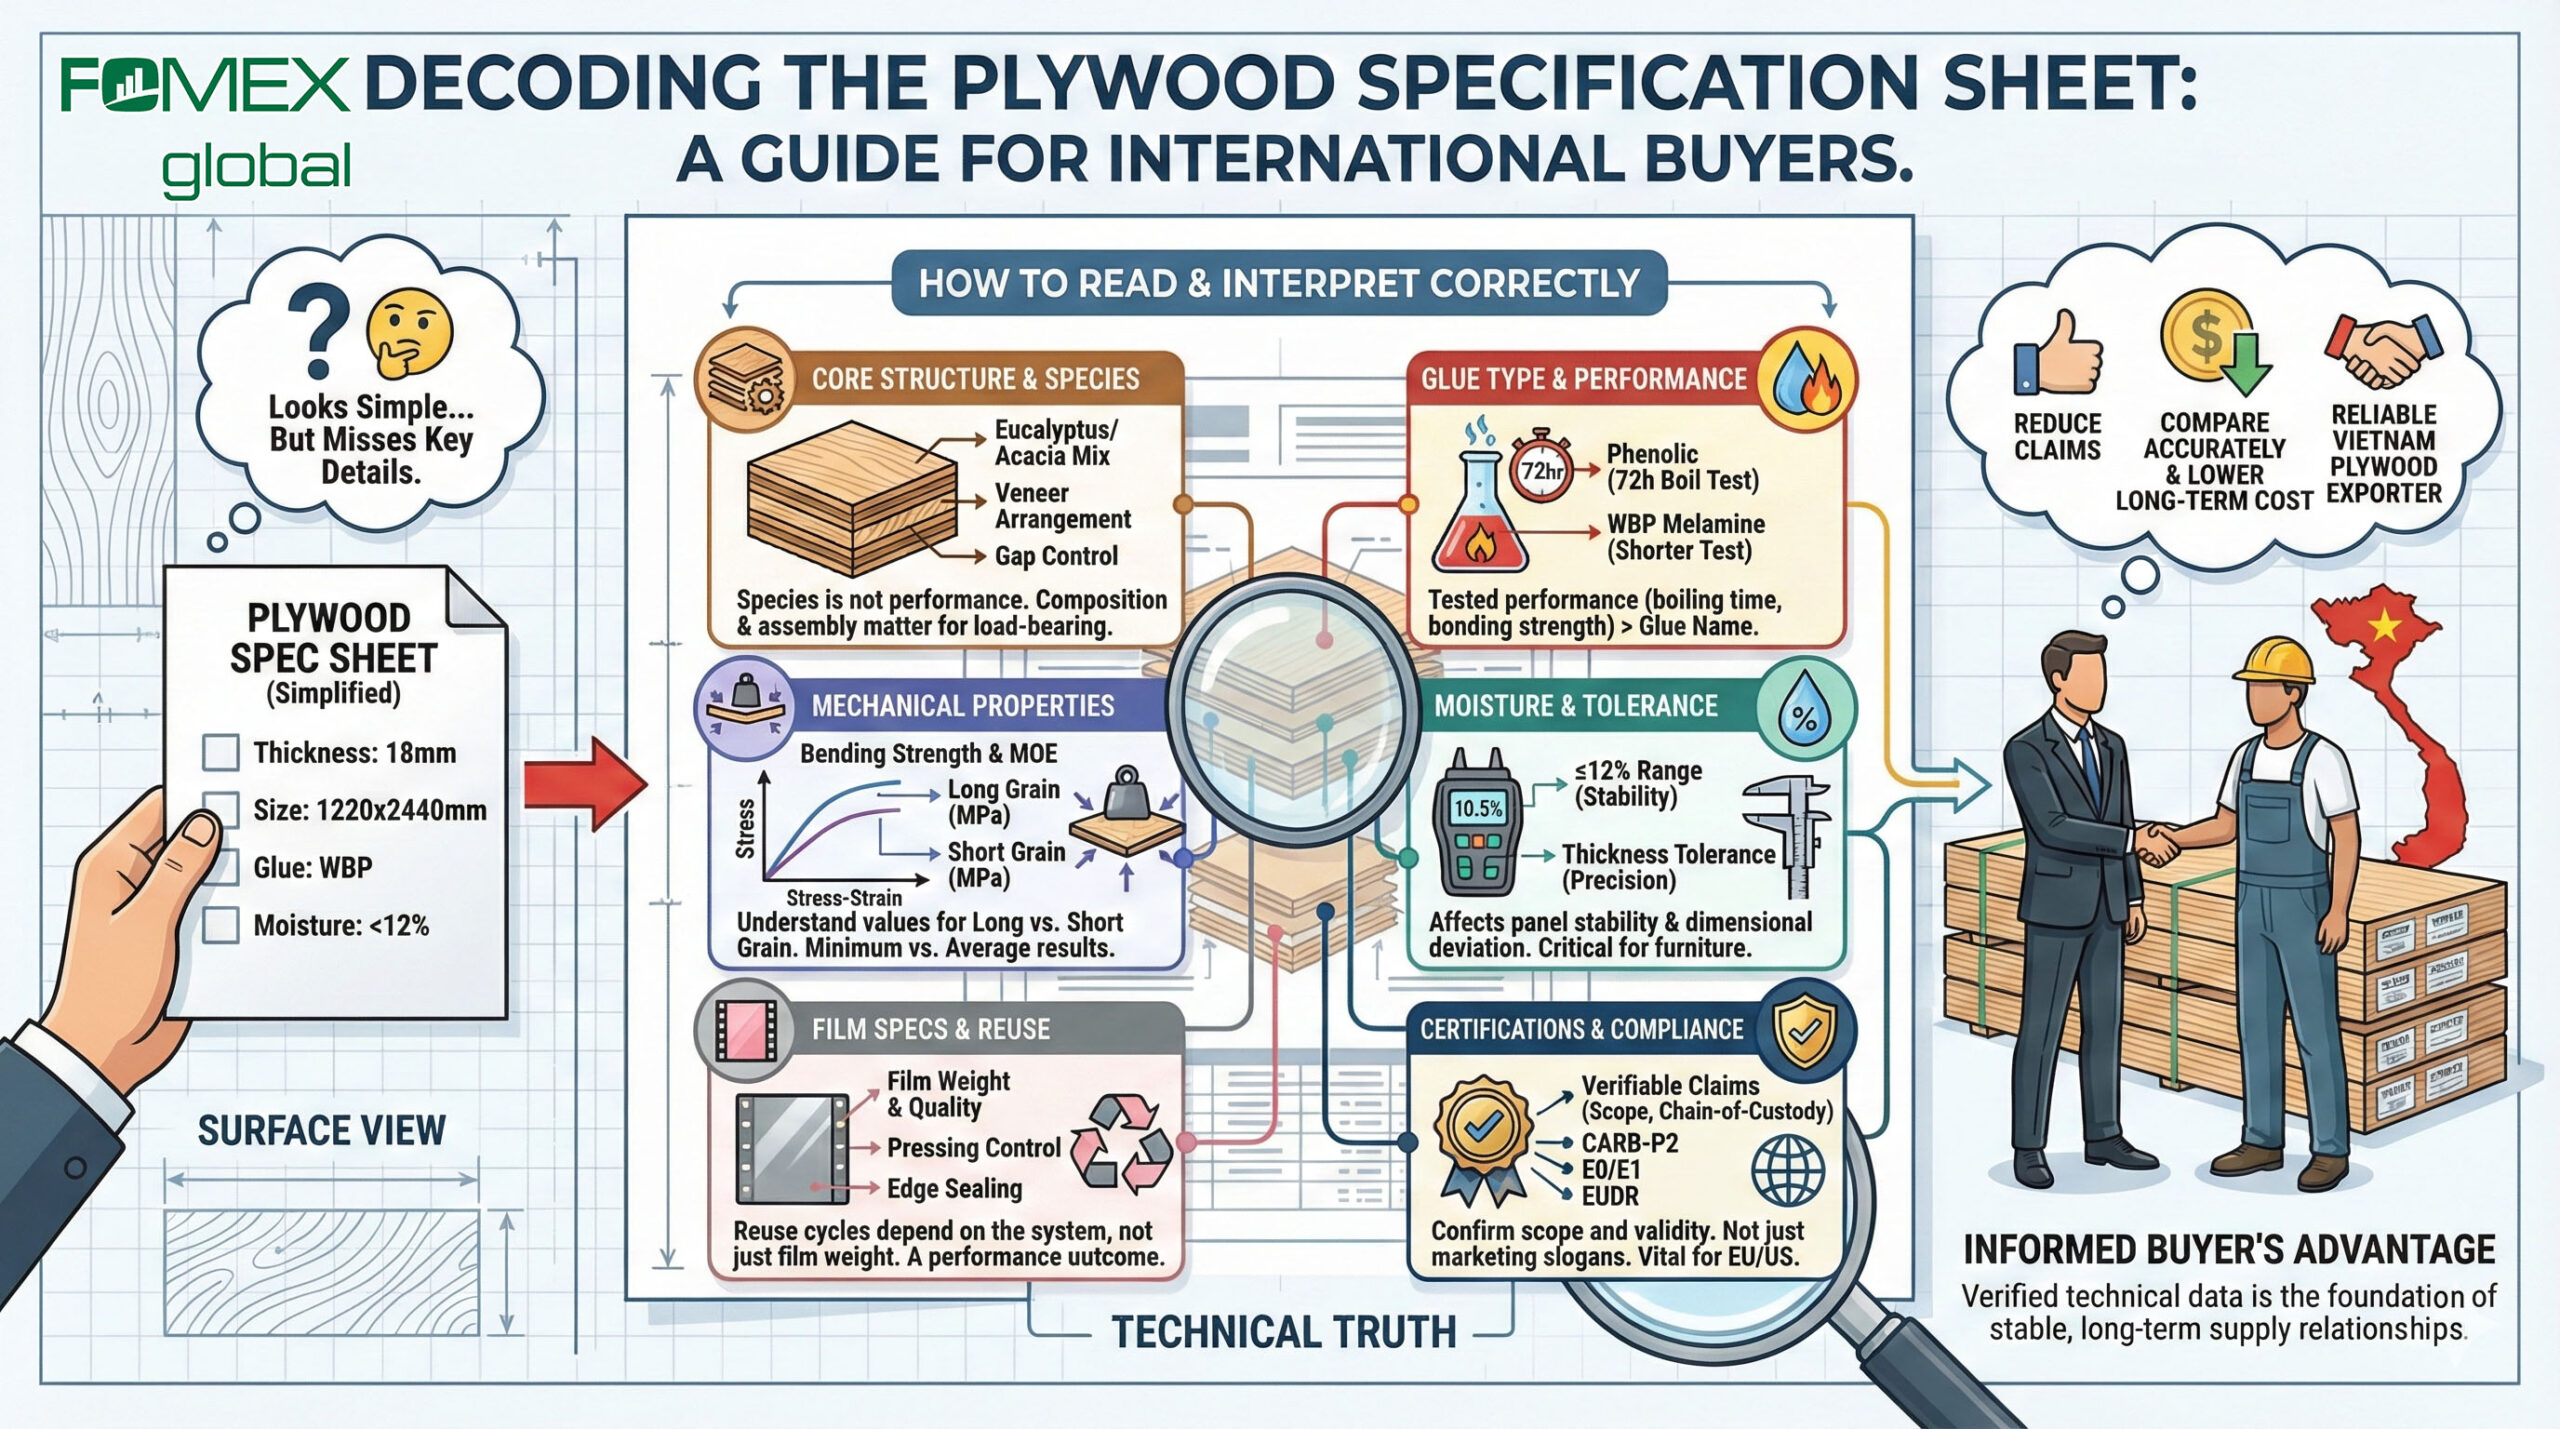
For many international buyers, a plywood specification sheet looks simple at first glance.
Thickness, size, glue type, moisture content – everything seems clearly listed.
However, most disputes in plywood import do not come from price or appearance,
but from misunderstood technical data.This guide explains how to read and interpret a plywood specification sheet correctly,
highlighting the key details importers often overlook.
Understanding plywood technical data helps buyers reduce claims,
compare suppliers accurately, and source from a reliable
Vietnam plywood exporter.

1. Why the Plywood Specification Sheet Matters

A plywood specification sheet is not a marketing document.
It is a technical contract reference that defines performance,
quality limits, and compliance standards.
For global buyers sourcing from a
Vietnam plywood manufacturer,
this document determines whether the product is suitable for furniture,
construction, or structural applications.

Importers who rely only on product photos or sample boards
often miss critical limits stated in the plywood specs explained in the data sheet.
These limits directly affect durability, reuse cycles, and long-term cost.

2. Core Structure and Wood Species

One of the first elements in any plywood technical data sheet is the core material.
Common options from a Vietnam plywood supplier include eucalyptus,
acacia, mixed hardwood, or commercial-grade combinations.

What buyers often miss is that the species listed does not automatically guarantee
mechanical performance.
Core composition, veneer arrangement, and gap control
are equally important.
This is especially relevant for buyers sourcing
high quality plywood Vietnam for load-bearing or repeat-use applications.

For a broader comparison of core structures and grades, see:

Understanding Plywood Grades & Quality Levels
.

3. Glue Type Is Not Just a Name

Glue systems are usually listed as MUF, WBP Melamine, or Phenolic.
Many importers stop reading at the glue name,
but a professional plywood specification sheet goes further.

What matters is the tested performance:
boiling time, bonding strength, and applicable standards.
For example, phenolic glue with a 72-hour boiling test
performs very differently from a melamine system with shorter resistance.

This distinction is critical for buyers sourcing
film faced plywood exporter Vietnam products
or structural panels for construction projects.

For a deeper explanation of glue performance indicators, refer to:
How Boiling Tests Affect Plywood Durability

4. Mechanical Properties: Reading Between the Numbers

Most plywood technical data sheets list bending strength and modulus of elasticity (MOE).
These values are essential for understanding how panels behave under load.

However, buyers often overlook whether values are listed for
long grain and short grain,
or whether the figures represent minimum limits or average test results.
This distinction matters when sourcing plywood for
construction projects or engineered furniture.

A reliable wholesale plywood supplier will clearly state
test methods and quality limits, not just headline numbers.

5. Moisture Content and Dimensional Tolerance

Moisture content is one of the most underestimated lines in a plywood specification sheet.
Values such as ≤12% are common, but buyers should understand
why this range exists and how it affects panel stability.

Thickness tolerance and dimensional deviation also deserve attention.
Small deviations may be acceptable for packaging panels,
but not for furniture manufacturing or calibrated plywood.

This is especially relevant for buyers sourcing
plywood for furniture manufacturers Vietnam
or precision interior applications.

Related reading:
Why Moisture Content Matters for Durability

6. Film Specifications and Reuse Expectations

For film faced plywood, the specification sheet usually lists film weight,
color, and surface type.
Importers often assume film weight alone defines reuse cycles.

In reality, reuse performance depends on the combination of
film quality, glue system, pressing control, and edge sealing.
A professional
sustainable plywood exporter
will treat reuse cycles as a performance outcome, not a promise.

For buyers comparing formwork panels, see:
Phenolic Film Weight & Concrete Finish Quality

7. Certifications and Compliance Statements

Certifications listed on a plywood specification sheet – such as FSC®, CARB-P2, E0/E1, or EUDR compliance – should be read as verifiable claims, not marketing slogans.

Professional importers sourcing from a
FSC certified plywood supplier
should always confirm scope, validity, and chain-of-custody alignment
with shipment documentation.

This is increasingly important for buyers in Europe and the US,
where regulatory scrutiny continues to increase.

Final Thoughts: Reading Specs Like a Professional Buyer

A plywood specification sheet tells a complete technical story – if you know how to read it. Beyond thickness and price, it defines structural behavior, durability, compliance, and long term cost.

For importers sourcing from a trusted Vietnam plywood exporter, understanding plywood specs explained clearly is the foundation of stable, long-term supply relationships.

Email: qc@fomexgroup.vn  |   WhatsApp: +84 877 034 666